Vane-type Oscillating Hydraulic Cylinder Body Housing Machining
Processing challenges
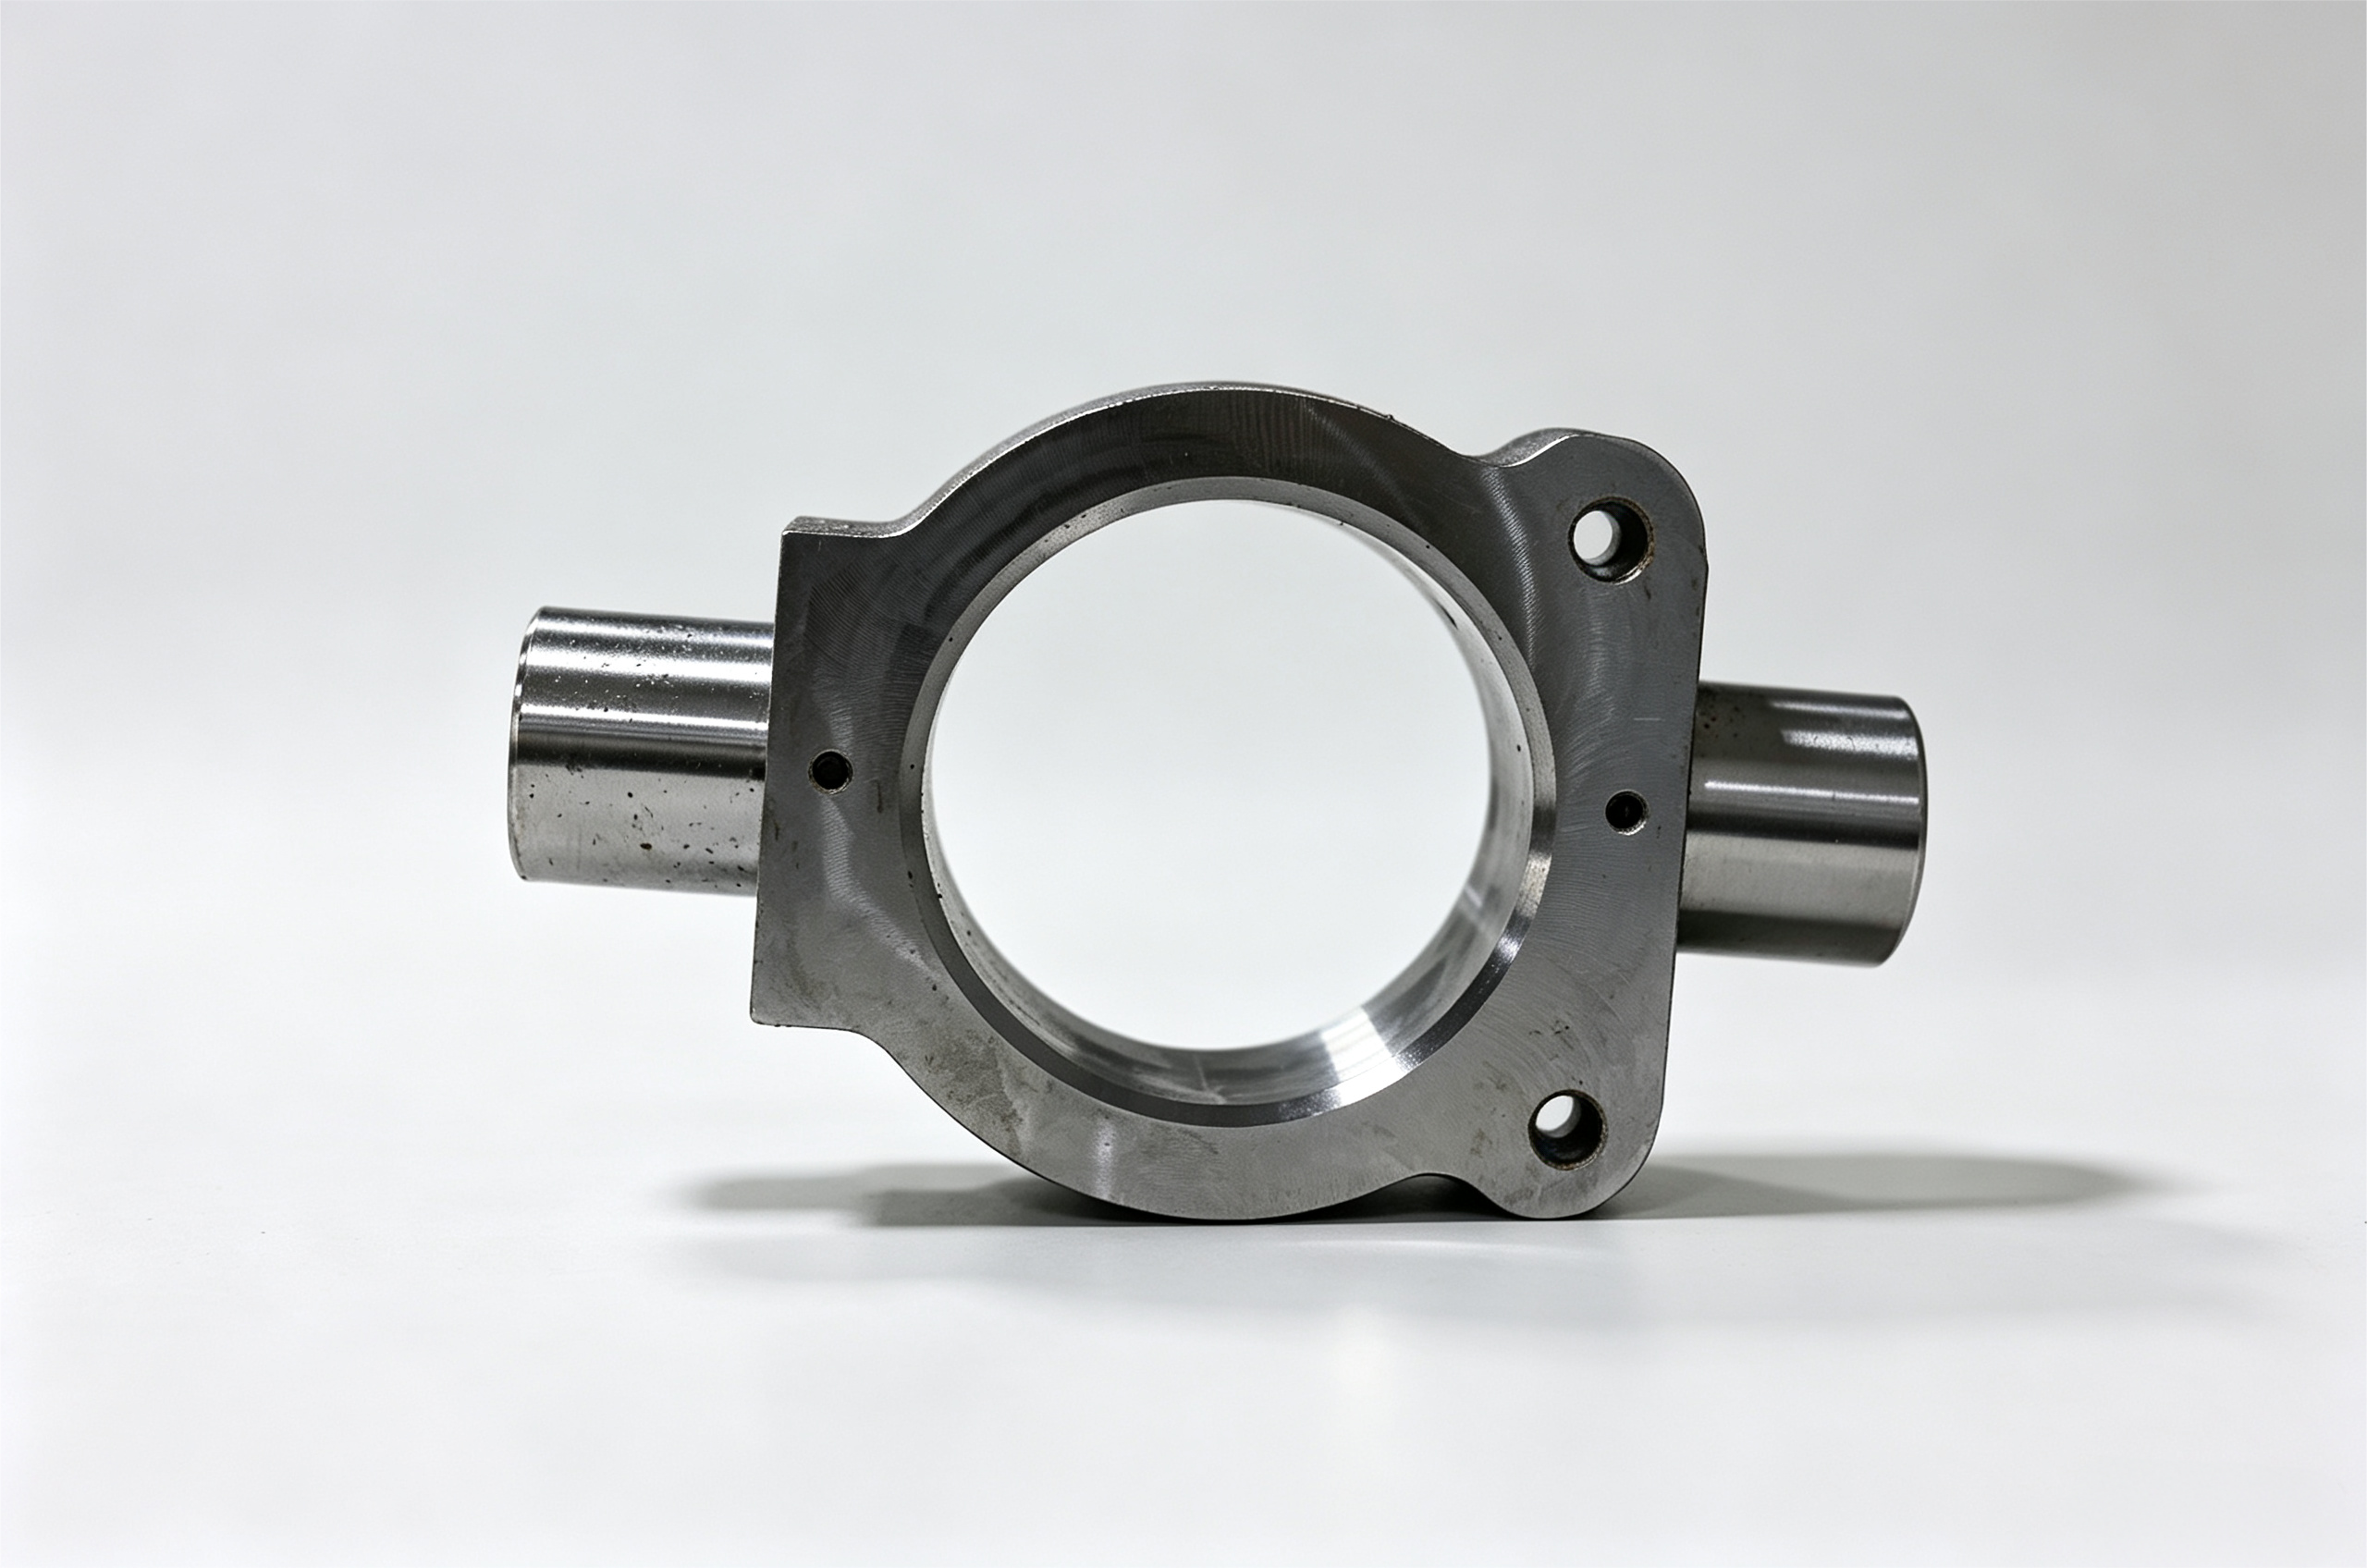
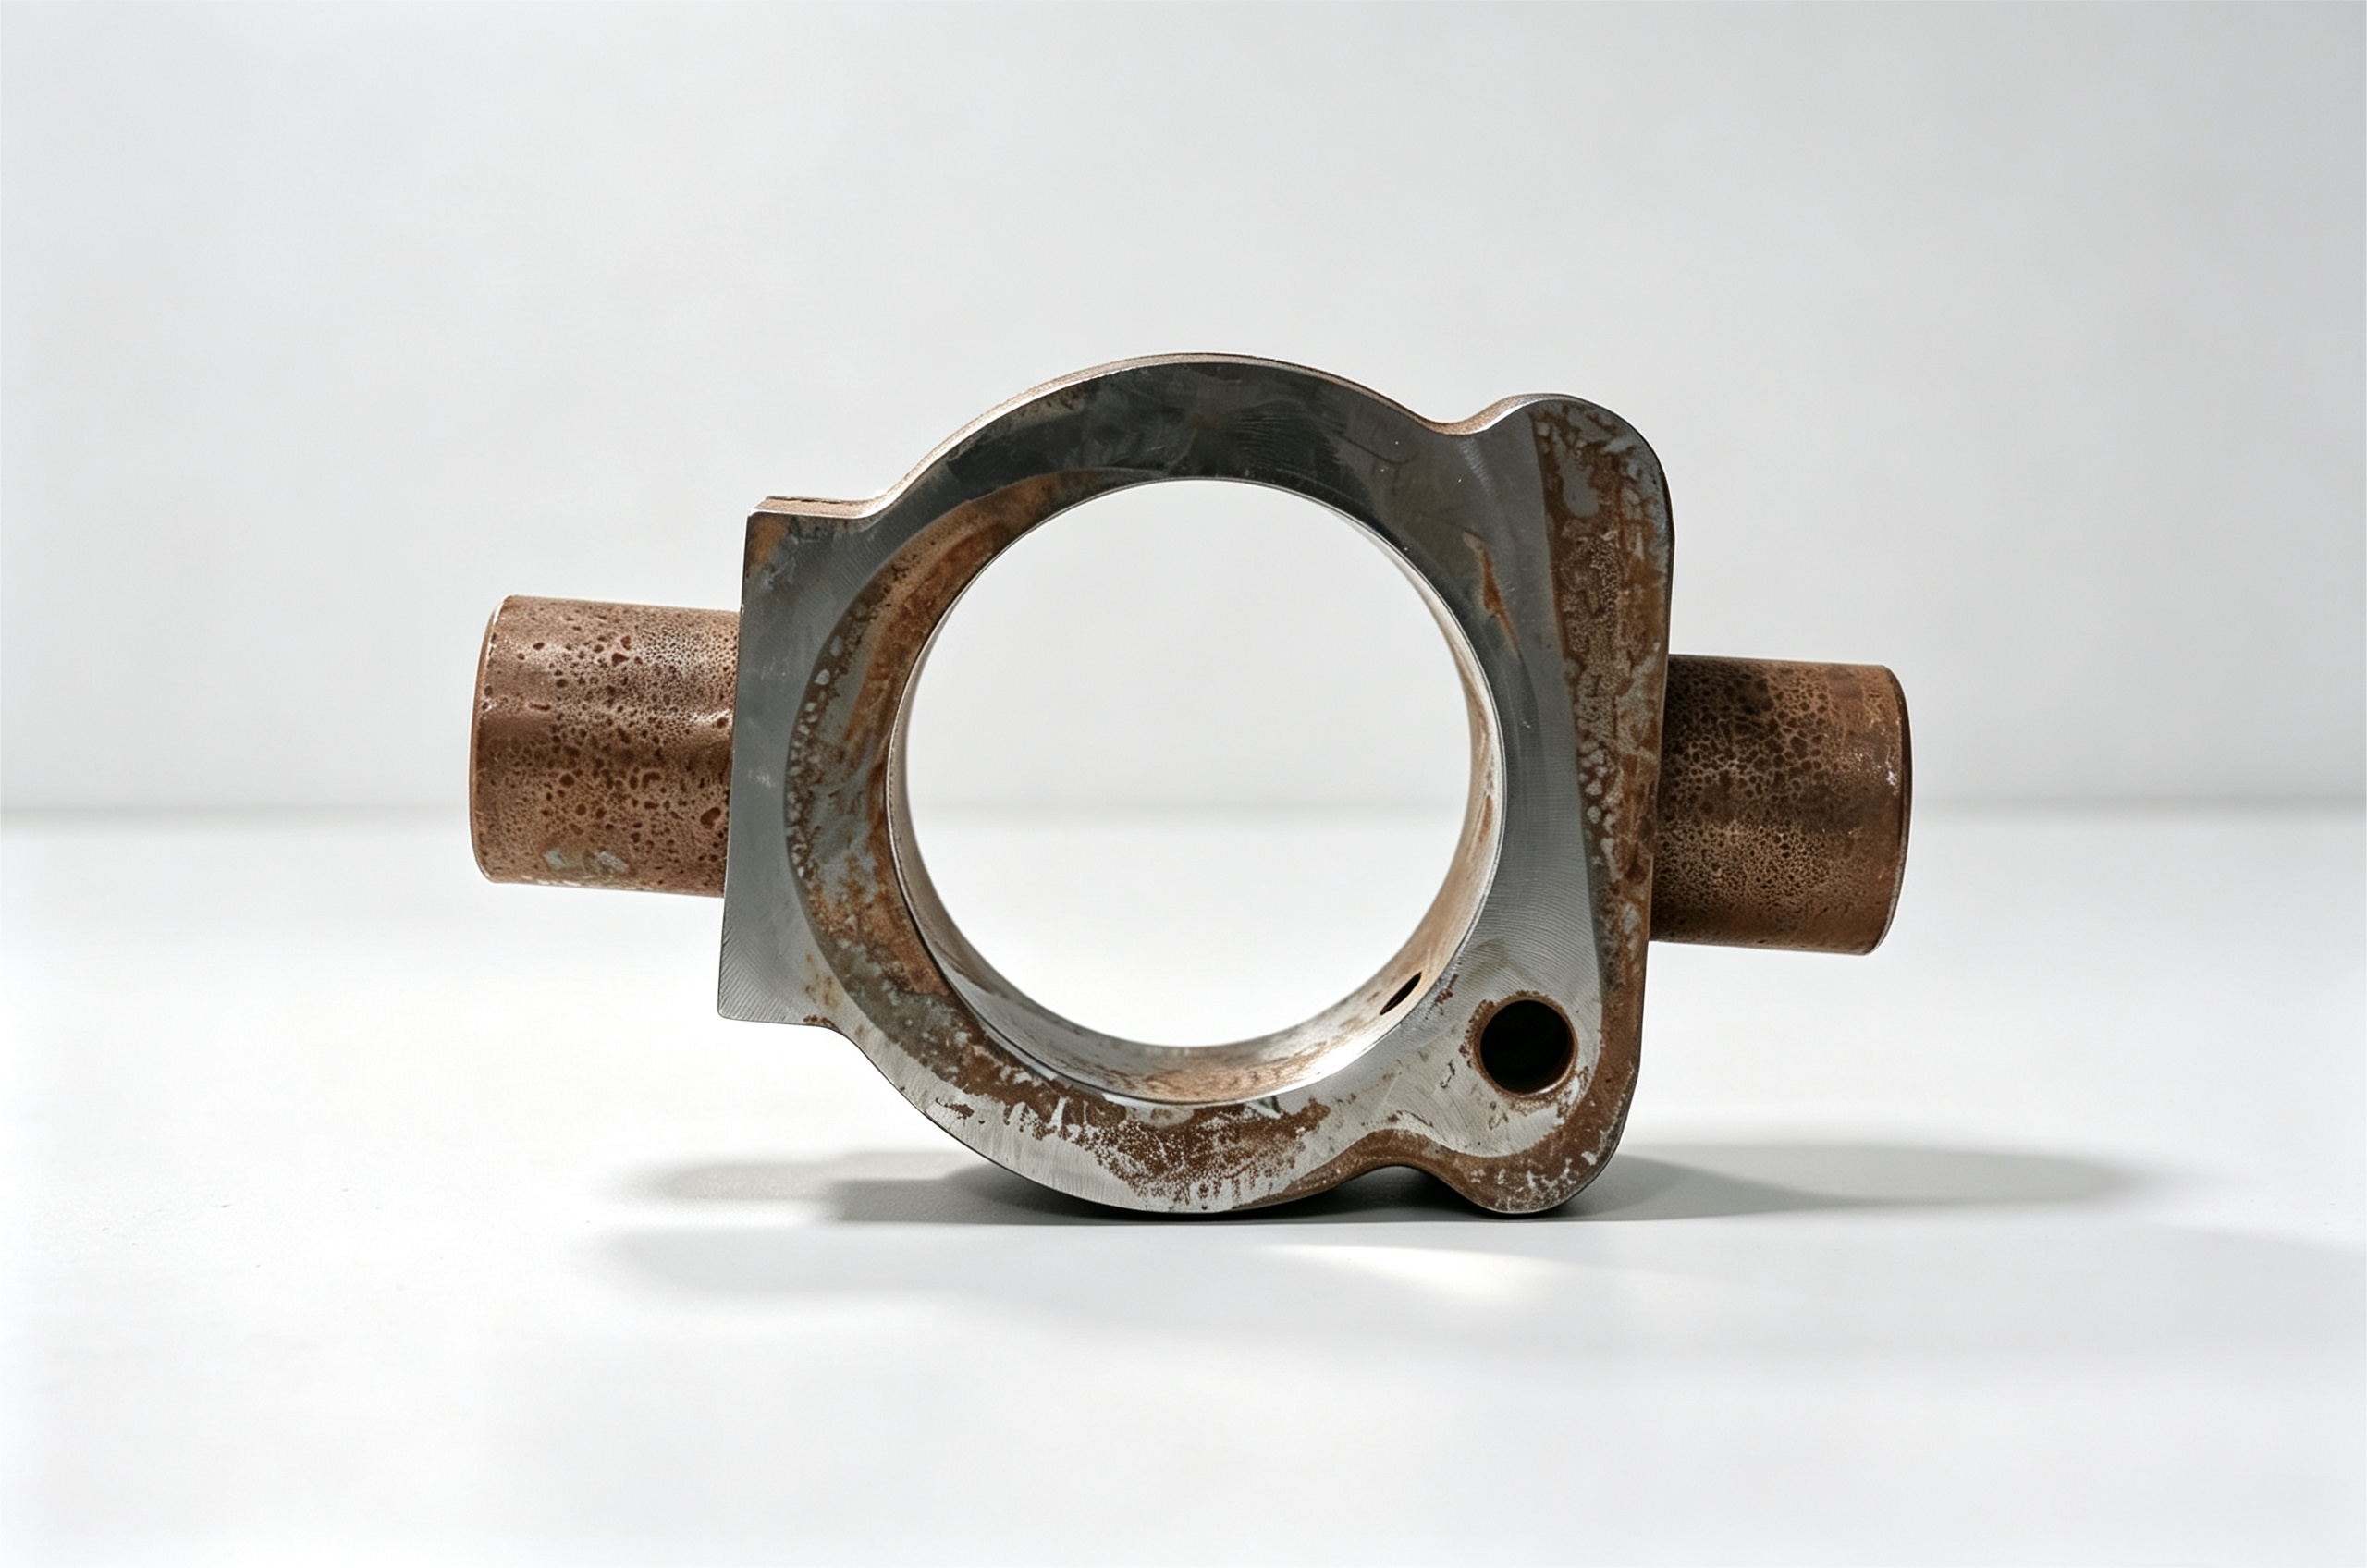
The oscillating hydraulic cylinder housing is a die-cast aluminum alloy component. It requires high bore accuracy to ensure precise fit with the rotor. The double-ear mounting surfaces must be machined to strict flatness and parallelity tolerances. Additionally, the positional accuracy of internal oil passages directly impacts hydraulic performance.
Solutions
High-precision CNC machining: roughing to remove casting allowances, followed by precision boring of the inner hole to meet tolerance requirements. Double ear mounting surfaces are processed using precision grinding. Oil passages are drilled with specialized drills and coordinate boring machines to ensure positional accuracy. Post-machining, CMM inspection verifies that all critical dimensions comply with drawing specifications.
Processed Results
- • Inner bore tolerance meets H7 fit requirements.
- • Bore axis mounting surface flatness ≤ 0.02mm
- • Oil passage hole position accuracy ±0.05mm
- • Surface roughness Ra1.6, meeting hydraulic sealing requirements.
- • Consistent mass production with a pass rate of 99.2%.
Technical Specifications
| Material | AC81 Die-Cast Aluminum Alloy |
| Inner bore tolerance | H7 Grade |
| Flatness | ≤0.02mm |
| Surface Roughness | Ra1.6 |
Need precision machining?
Submit your drawings, 3D files, or product requirements. Our engineering team will provide a professional machining solution.